Capability 03 / Fabrication
Fabrication and welding
Sheet and plate cut, folded and welded under the same roof as the machine shop, so a frame can be stress relieved, machined after welding and finished without leaving our hands.
- mm laser bed
- 3,000
- tonne press brake
- 170
- welding bays
- 6
- tonne crane, under hook
- 2
The kit
Cut, fold, weld, machine.
Nested on the laser straight from your DXF, folded on a CNC brake with the bend allowances proven on a first-off, then welded in fixtures we make ourselves.
| Process | Equipment | Capacity |
|---|---|---|
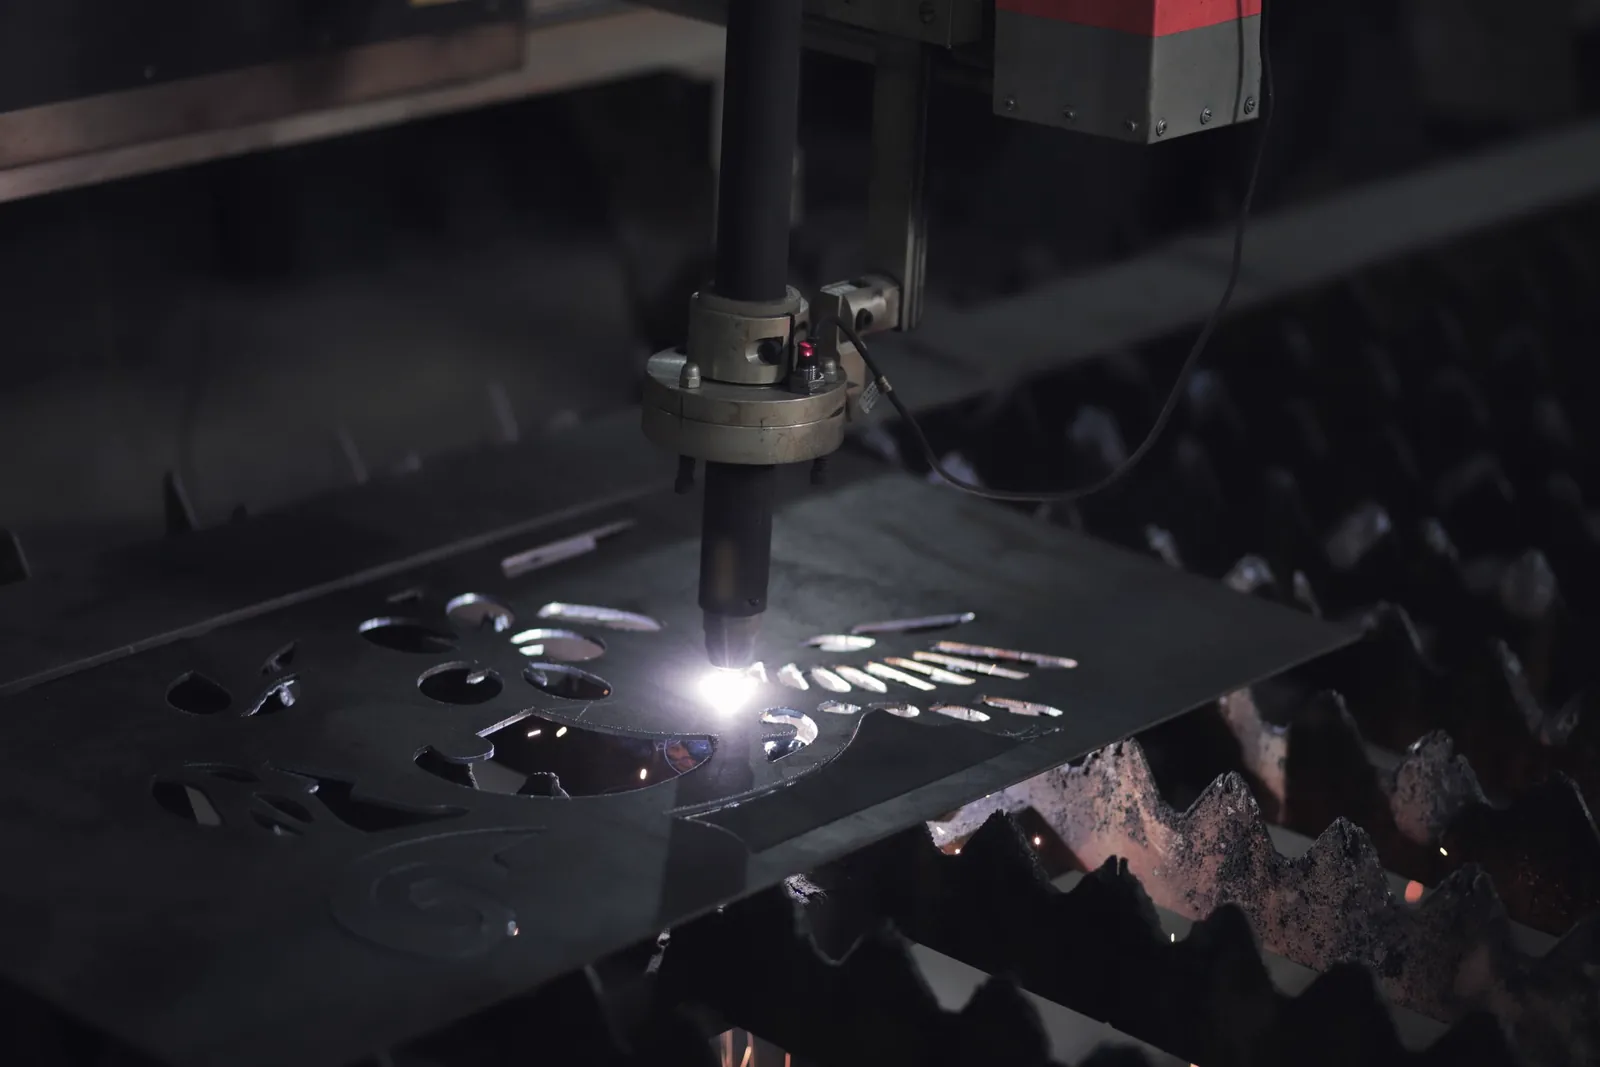
| Laser cutting | Fibre laser, 6 kW | 3,000 × 1,500 mm sheet; mild steel to 20 mm, stainless to 15 mm, aluminium to 12 mm |
| Plasma cutting | CNC plasma table | Plate to 40 mm, 3,000 × 1,500 mm |
| Folding | CNC press brake, 170 t | 3,100 mm long; mild steel to 10 mm |
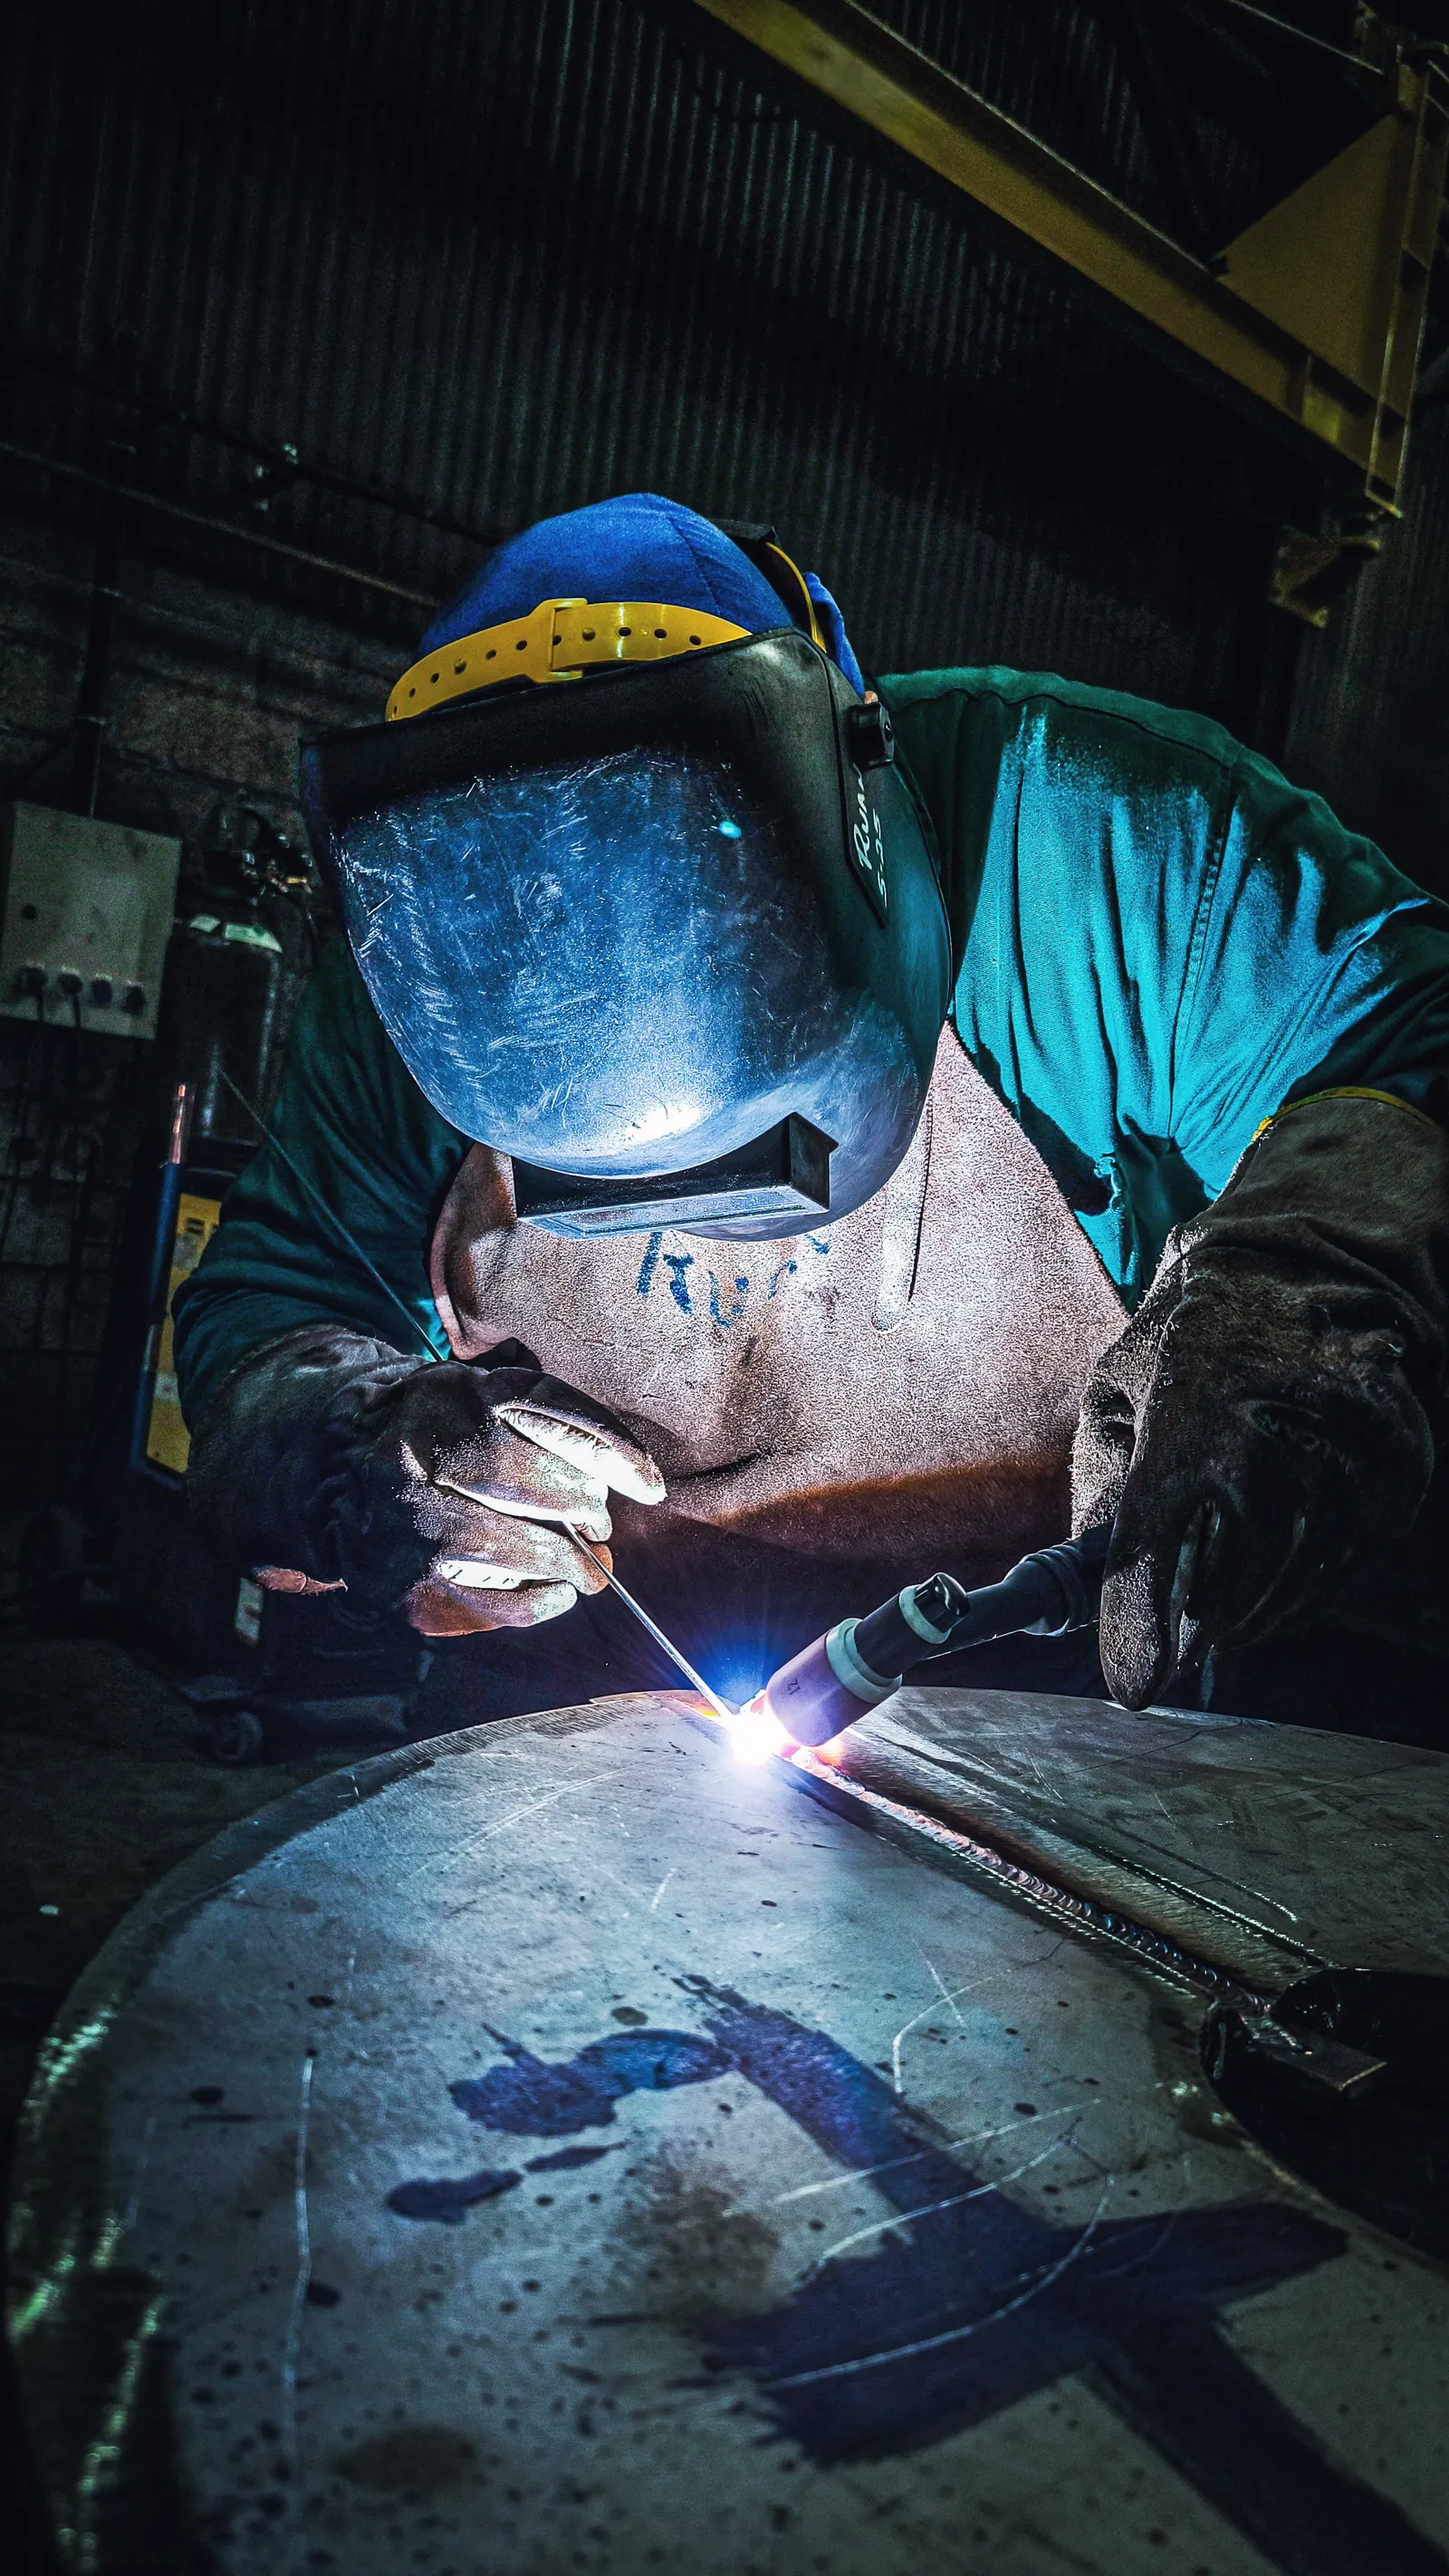
| Welding | MIG and TIG, 6 bays | Steel, stainless and aluminium; pulsed TIG for thin stainless |
| Sections | Bandsaw and drilling line | Box, angle, channel and tube to 400 mm |
What we hold
Square, flat and to size.
Welding to the symbols and specification on your drawing, with weld maps and inspection records kept with the job.
| Parameter | Figure |
|---|---|
| Cut profiles | ±0.1 mm (laser), ±0.5 mm (plasma) |
| Folded parts | ±0.2 mm on flanges, ±0.5° on angles |
| Welded fabrications | ±1 mm under 2 m before machining |
| Largest fabrication | 4 × 2 × 2 m, 2 t |
| Weld inspection | Visual to your specification; dye penetrant in-house; other testing through partners |
| After welding | Stress relief through partners; machined in-house |
Machined weldments
One supplier, from plate to finished frame.
Most fabrications that come to us need machining after welding: bearing faces, datum pads, tapped holes. Doing both here takes a supplier, two deliveries and a week out of the job, and puts one name on the inspection report.